
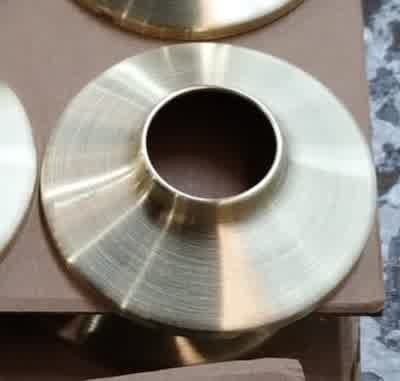
Decorative metal finishing requires more than simply choosing an abrasive product.
 Ed SlinskyAppliance and architectural manufacturers, as well as other fabricators producing appearance-critical metal components, often need specialized, reproducible scratch patterns that help distinguish finished products. The abrasive selected for the process directly affects both production efficiency and visual consistency.
Metal finishers can choose from a broad range of abrasive technologies, including coated belts, bonded wheels, non-woven products, and bristle products. Each category offers different performance characteristics. For applications that require a controlled decorative finish, non-woven flap brushes and interleaf wheel configurations provide a combination of conformability, finishing consistency, and process flexibility.
Drawing on 30 years of field experience in industrial metal finishing, this article examines the materials, construction, and operating variables that affect the performance of non-woven flap brushes and interleaf wheels.
Understanding Non-Woven Abrasive Materials
 Non-woven abrasives are an important product category used in surface preparation and decorative finishing. Common non-woven abrasive classifications include:
- Surface-conditioning media
- Flat stock, often described as buff-and-blend material
- Unitized wheels
- Convolute wheels
These products are engineered using synthetic nylon filaments that vary in length and denier, or fiber thickness. The fiber blend's characteristics influence the density, yield, and stiffness of the finished abrasive material. Those differences help create distinct performance levels, including General Purpose (GP) materials for lighter-duty applications and High Strength (HS) materials for heavier-duty work.
As automated and CNC finishing lines continue to expand, manufacturers increasingly require abrasive products that can maintain performance through longer production runs. Higher-durability non-woven abrasives can minimize wheel wear, reduce downtime from wheel changes, and support more consistent cut rates over time.
Building the Non-Woven Web
The consistency of a non-woven abrasive begins with the manufacturing process. Buff-and-blend material is primarily produced through air-laid web formation, which creates a high-loft, porous structure composed of randomly oriented nylon fibers.
The process can be summarized as:
Air-laid web formation → Liquid resin and grain application → Controlled thermal curing → Conversion into flap strips
After the fiber matrix forms, the process applies liquid resin and abrasive grain. The resin system may use phenolic or polyurethane resins combined with abrasive minerals, typically aluminum oxide or zirconia alumina.
Process control during resin application and thermal curing is important to maintaining consistency across the jumbo roll. Ambient temperature and relative humidity affect the application and curing environment, while cure time and resin viscosity influence the finished web’s flexibility and cut rate. Controlling these variables helps support more uniform grain density and more consistent finishing performance from the converted abrasive product.
How Non-Woven Flap Brushes Work
A non-woven flap brush is constructed by radially bonding slit strips of buff-and-blend web around a central core. As the tool contacts the workpiece, the web structure allows the brush to conform to the part while helping maintain its geometry.
Several construction variables influence finishing performance:
- Wheel density: Increasing flap count stiffens the brush, promoting a more aggressive cut and higher luster. Lower-density brushes conform better to irregular workpieces.
- Web loft: The loft of the non-woven material affects the tool’s flexibility and contact behavior.
- Web orientation: Web orientation affects how the brush contacts and conforms to the workpiece.
The combination of these variables enables finishers to tailor the brush to the part geometry and desired surface appearance.
Interleaf Wheels Combine Cut and Finish Refinement
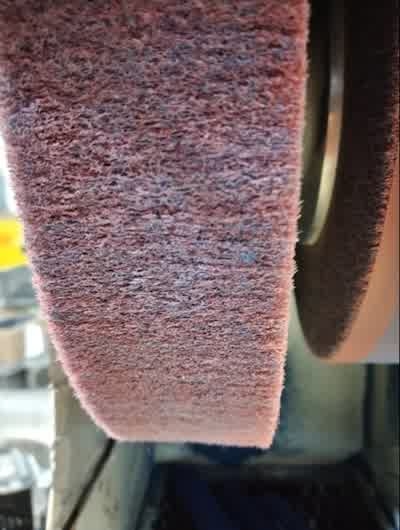 When an application requires increased stock removal while maintaining a refined surface finish, an interleaf wheel, also called a combi wheel, can be used. These tools combine alternating flaps of non-woven web and flexible coated abrasives, commonly in predetermined ratios such as 1:1.
The coated-abrasive portion provides additional cutting action, while the non-woven material supports a more refined finishing effect. This combination can be useful when a finishing process requires both stock removal and a controlled decorative appearance.
The coated-abrasive flaps incorporate several important components:
- Backing fabric: Durable X-weight cotton backing provides tensile strength, tear resistance, and the conformability needed to track complex contours without creasing.
- Grain coating: A close-coat application of synthetic mineral covers most of the backing surface. The distribution of contact force across numerous grain points helps produce a uniform scratch depth and reduce deep, stray scratches.
- Abrasive mineral: Aluminum oxide and zirconia alumina offer different cutting characteristics for different finishing requirements.
Aluminum oxide offers toughness and self-sharpening characteristics suited to general stainless-steel and non-ferrous finishing. Zirconia alumina provides microfracturing characteristics suited to higher-pressure stock removal and can produce distinct scratch characteristics on harder alloys.
Controlling the Decorative Finish: Achieving a target arithmetic average surface roughness (Ra) and a specific visual scratch pattern requires attention to several process variables. Among the most important are flap density, grit sequencing, speed, and pressure.
Flap Density: Increasing flap count stiffens the brush, which promotes a more aggressive cut and higher luster. Reducing flap density increases conformity, allowing the brush to follow irregular surfaces better.
Grit Sequencing: The combination of coated-abrasive grit and non-woven material affects the final visual result. For example, pairing a 120-grit coated-abrasive flap with a medium non-woven web produces a distinct directional grain. Pairing a 180-grit coated-abrasive flap with the non-woven material produces a satin finish.
These examples demonstrate why abrasive selection should be based on the required appearance rather than grit alone. The desired scratch pattern, finish level, and production objective should guide the selection of abrasive mineral, grit, web construction, and flap configuration.
Speed and Pressure: Peripheral speed, commonly expressed in surface feet per minute (SFPM), affects how the nylon fibers flex during finishing. Maintaining the appropriate peripheral speed helps the fibers perform as intended and helps prevent thermal smearing of the web resin onto the metallic substrate.
Pressure must also be managed as part of the process. Together, speed and pressure influence the finishing action, surface appearance, and consistency of the result.
Establishing a Repeatable Process
Non-woven flap brushes and interleaf wheels give finishers a practical way to balance conformity, cutting action, and decorative surface appearance. The appropriate combination of web loft, backing flexibility, abrasive mineral chemistry, and flap ratio helps manufacturers establish repeatable, high-efficiency finishing processes across a range of metal substrates.
For appearance-critical finishing, the objective is to match the abrasive construction and operating conditions to the target surface. By controlling material selection, wheel design, grit combination, peripheral speed, and pressure, metal finishers can produce consistent decorative finishes while supporting efficient production.
Ed Sklinsky, Vice President of Sales at Klingspor Abrasives. Please visit https://www.klingspor.com.