
For many plating shops, the pressure is familiar: customers want shorter lead times, production managers want more throughput, and quality teams want fewer rejects.
 Jason PottsToo often, those goals seem at odds. Speed up the line and reject rates climb. Slow things down and production targets suffer.
But according to industry veterans Jason Potts of Hubbard-Hall and Shane Moore of Pavco, that tradeoff is not as inevitable as many finishers believe.
In fact, some of the most costly reject problems they encounter are not caused by chemistry failures at all. Instead, they stem from process drift, overlooked maintenance, contaminated rinses, incoming part changes, or seemingly minor adjustments made with the best of intentions.
“We always hear that the bath is bad,” says Potts, Hubbard-Hall’s regional sales manager with more than 30 years of metal finishing experience. “But I go back to the beginning. I start at the very front of the line. Let’s make sure we’re getting clean parts first.”
That philosophy has helped the Hubbard-Hall and Pavco teams solve problems that were costing shops significant money in scrap, rework, and lost production.
Images courtesy of Pavco, https://pavco.com
Sometimes the Fix Is Simpler Than Anyone Thinks
 Shane MooreMoore recalls one decorative finishing operation that believed it had a persistent trivalent chromium plating problem.
The customer had decided to keep its chloride-based trivalent chromium bath heated to approximately 140°F at all times. The reasoning seemed logical. Keeping the tank hot would allow salts to dissolve faster and eliminate the wait associated with heating and cooling cycles.
The shop thought everything looked good except for a recurring brown spot on plated parts. When Moore investigated, he found something surprising.
“They said everything looks great except for this one brown spot that we keep getting,” Moore says. “I took the part back to the lab and measured it. It turns out the only chromium on the entire part was that little brown spot they were complaining about.”
The solution?
“Turn the heater off,” he says, an example that highlights a lesson both experts emphasize repeatedly: diagnosis must come before correction.
Far too often, platers try to solve symptoms instead of causes.
Watch the video interview: https://www.hubbardhall.com/proof/podcasts/reducing-rejects-without-slowing-production
The Hidden Cost of Running Too Fast
Every shop wants more throughput. The problem occurs when increasing production speed compromises process fundamentals.
Potts says line-speed changes frequently create unintended consequences throughout the finishing cycle.
“When the line is sped up, you’re spending less time in your cleaners,” he says. “You’re trying to get the work out. Even if you get the parts clean, then you get into the plating bath, and because you’re going faster, you have less time there. Maybe you’re not meeting thickness spec, or you’re getting roughness because you try to plate fast, or burning.”
The impact often starts much earlier than the plating tank. Moore points to acid activation stages where shortened immersion times may leave weld scale or oxides partially intact. The remaining contamination may not become obvious until much later in the process.
“I want to quote Randy DiSano,” Potts says. “He says, ‘The Hull cell is the EKG of the bath.’”
“It may remove some of it, but leave enough behind where you see that pattern at the end of the line,” Moore says. “Then you have to trace it back to where that pattern came from.”
The result is a frustrating reality many finishers know well: by the time defects are discovered, hundreds or even thousands of additional parts may already be moving through the system.
On automatic lines especially, defects often remain invisible until parts reach unracking or final inspection.
Rejects Often Begin Before Parts Reach the Line
 While finishing engineers frequently focus on plating chemistry, Potts and Moore say many quality issues originate with incoming parts.
A customer may switch machining oils without notifying the plater. Another supplier may ship parts that have sat in storage long enough to develop rust. Contamination from handling, food residue, fingerprints, or unexpected lubricants can all trigger adhesion and appearance problems.
“The manufacturer of the part does not notify the applicator that there’s been a change,” Potts says. “Whether it’s oil, different types of material, parts sat around and became rusty. There are so many things that you see parts coming in.”
Moore recalls one case where a shop suddenly began experiencing unexplained reject problems. After investigation, the team discovered the customer had switched machining fluids.
“They forgot to mention it was full of paraffin wax,” Moore says.
The finishing line’s cleaning process had not changed, but the new lubricant required significantly higher cleaner temperatures for effective removal.
“They didn’t have their soak cleaner and electric cleaner temperatures high enough to melt that wax,” he explains. “So instant rejects.”
Potts laughs when the topic comes up.
“Paraffin wax is a monster,” he says, and most platers would agree.
The Danger of Quick Fixes
When problems develop, operators understandably want immediate solutions. Unfortunately, quick fixes can create bigger problems.
One of the most common mistakes both men see is over-addition of process chemicals. Rather than identifying root causes, operators often compensate with extra brighteners, wetting agents, or additives.
“Over-adding is a short-term fix when the problem could be somewhere else,” Potts says.
Moore sees the same pattern. A shop may experience haze, contamination, or appearance issues and respond by adding more brightener to the bath.
“They add more and more brightener,” Moore says. “Then if you accumulate too much brightener, you have problems down the line after that.”
Eventually, one issue becomes two. A contamination problem evolves into a contamination problem plus an additive-control problem.
Another common shortcut involves electrical settings. Potts has seen facilities adjust rectifiers to compensate for unrelated process issues rather than addressing the root cause.
Those changes may temporarily hide symptoms but often create additional quality challenges elsewhere on the line.
Learning to Spot Trouble Early
The best reject is the one that never happens. That requires identifying issues before parts reach final inspection.
For both Potts and Moore, the Hull cell remains one of the industry’s most valuable diagnostic tools.
“It plays the panel from a very high current density to a very low current density,” Moore says. “A lot of times you’ll spot a problem before it actually gets into that area, so you can address it then before it becomes an issue.”
Potts is equally enthusiastic.
“I want to quote Randy DiSano,” he says. “He says, ‘The Hull cell is the EKG of the bath.’”
“Everything that you’re dragging out that you’re keeping from accumulating in the beginning, you’re putting that right back into the tank,” Moore says.
Beyond laboratory testing, simple visual observations remain surprisingly effective. Operators should routinely watch for:
- Oil on rinse tanks.
- Unusual surface appearance leaving cleaners.
- Contaminated acid tanks.
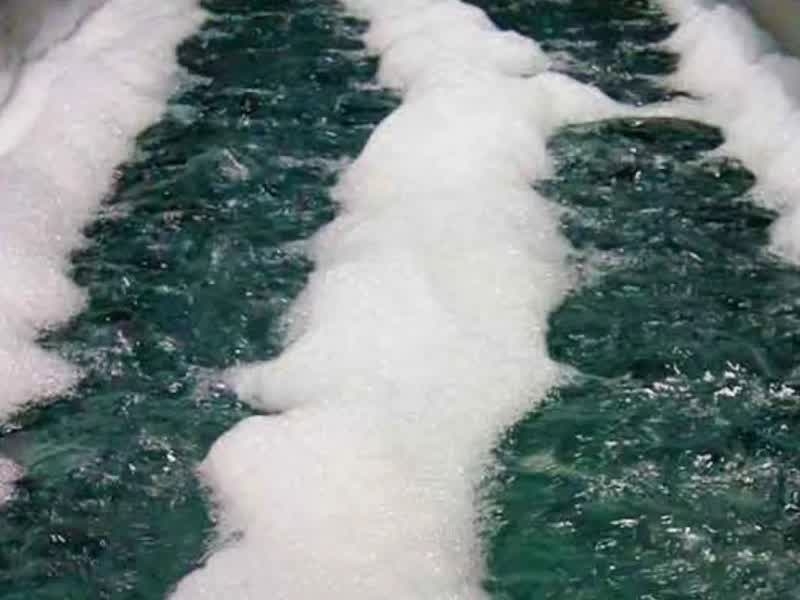
- Abnormal foam conditions.
- Water-break failures.
- Poor overflow performance.
- Changes in solution color.
Even something as simple as a tank that suddenly lacks its normal foam pattern can reveal an important clue.
“If there’s zero foam in the tank,” Moore says, “that could be an issue too.”
Why Rinsing Still Matters
Few process steps receive less attention and more blame than rinsing. Yet both experts consider rinsing one of the most important factors affecting reject rates.
Potts notes that seasonal conditions alone can influence rinsing effectiveness. In northern climates, winter rinse temperatures can drop significantly compared with summer operations.
“I look at it this way,” Potts says. “When you wash your hands, if you try to get the soap off in cold water, it doesn’t come off very easily. But if you warm that water up, it really comes off.”
The analogy resonates because it reflects what happens in plating operations. Colder rinses reduce contaminant removal and increase the risk of dragout-related problems. Moore warns against another common issue: overreliance on recovery rinses.
“The soap cleaners are starting to celebrate birthdays,” Moore jokes. “They should never celebrate a birthday.”
Many operations use dead rinse systems to reduce water consumption and improve chemical recovery. While that can save money, it also creates risks if not managed correctly.
“Everything that you’re dragging out that you’re keeping from accumulating in the beginning, you’re putting that right back into the tank,” Moore says.
The result can be accelerated buildup of organics, metallic contaminants, and other unwanted materials that ultimately affect bath performance.
Process Drift: The Silent Quality Killer
When discussing chronic reject problems, both experts repeatedly return to one phrase: process drift.
The concept sounds simple, but its effects can be devastating. Small changes accumulate over time. An operator shortens a cleaning cycle slightly. Another extends maintenance intervals. Production increases while staffing remains unchanged.
Each adjustment appears harmless by itself. Collectively, they move the process farther away from optimal conditions.
“One day you come into the shop and decide you’re going to clean for five minutes,” Potts says. “Then you go to four minutes. Well, then you’re going to change everything else down the line.”
Moore sees similar issues with preventive maintenance programs. A cleaner scheduled for routine dumping remains in service longer. Carbon treatments are skipped. Filters are changed less frequently. Production demands gradually take precedence over maintenance activities.
“The soap cleaners are starting to celebrate birthdays,” Moore jokes. “They should never celebrate a birthday.”
The humor carries an important message: finishing systems require discipline to remain stable.
The Value of Fresh Eyes
One theme surfaced repeatedly throughout the discussion: many shops become so familiar with their own operations that they no longer notice developing problems.
Operators see the same equipment every day. Managers walk the same path through the line every morning. Conditions that would stand out immediately to an outsider become normal.
That’s why Potts and Moore are strong advocates for line audits and outside evaluations. During installations and troubleshooting visits, both professionals routinely inspect far more than the immediate complaint.
They review cleaners, rinses, rectifiers, anodes, filtration systems, electrical connections, overflow rates, agitation systems, maintenance records, and operating procedures.
“A lot of times they get so immersed in looking at the same thing every day,” Moore says, “they don’t realize maybe something could be tweaked or improved.”
“If I go into a call and someone says they’re having a problem, I don’t want to just look at the bath,” he says. “I want to look at everything.”
The collaborative relationship between Hubbard-Hall and Pavco adds another layer of expertise. Rather than focusing solely on plating chemistry or solely on cleaning chemistry, the teams evaluate the entire process.
“We have two sides of expertise,” Potts says. “Pavco with the plating side, Hubbard-Hall with the cleaning side. A lot of times it’s not just the chemistry.”
The combination can speed up troubleshooting and deliver faster solutions.
“We can bounce ideas off each other and come to a solution much quicker that way,” Moore adds.
Partnership Over Product
Perhaps the biggest takeaway from the discussion is that successful troubleshooting rarely starts with a drum of chemistry. It starts with a systematic evaluation of the process.
One recent joint project involved conversion of an alkaline zinc operation that had been struggling with chelation-related waste-treatment challenges. Working together, the Hubbard-Hall and Pavco teams evaluated the process, improved cleaning performance, converted the plating chemistry, and ultimately increased throughput while helping the customer run fuller production racks.
For Potts and Moore, those successes reflect a broader philosophy.
“We’ve become a partner with all of our customers,” Moore says. “It’s not just that we supply them with the chemistry.”
Potts echoes that sentiment.
“If I go into a call and someone says they’re having a problem, I don’t want to just look at the bath,” he says. “I want to look at everything.”
In an industry where delivery schedules are shrinking, and quality expectations continue to rise, that comprehensive approach may be more valuable than ever.
The good news for finishers is that reducing rejects doesn’t necessarily require slowing production. More often, it requires understanding the process, maintaining discipline, recognizing early warning signs, and being willing to investigate root causes before reaching for quick fixes.
As Potts and Moore have repeatedly found, the fastest path to better throughput is often fixing the small things everyone else has learned to overlook.
Visit https://www.hubbardhall.com and https://pavco.com.